



Uitgebreide Gids voor Selca CNC G51 Offset & Coördinaterotatie – Programexample
Ingediend door: Brian
Tekening/Afbeelding
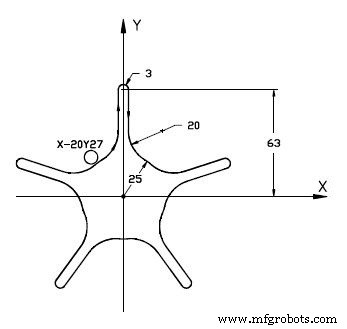
CNC-programma
N1 [PROFILE 3 N2 $1M0X-105.I103.Y-63.7J69.3 N3 G17 N4 O1 N5 T1 N6 F1000S1200M3 N7 Z100R N8 X-20Y27R N9 Z2R N10 Z-10 N11 G49I2 N12 G41K2 N13 L=1 N14 G20X0Y0I-25 N15 G21I10 N16 G13X-3J90 N17 G20X0Y63I-3 N18 G13J-90 N19 G21 N20 G51J-72I N21 L1K4 N22 G51J0 N23 G50 N24 G20X0Y0I-25 N25 G40X-20Y27K2 N26 Z100R N27 M30
Uitgebreide G&M Codes Referentie voor Fagor 8070 CNC Machine
Selca CNC Programmeeruitdaging – Geavanceerde Code Oefening
CNC machine
- Fanuc G75 freescyclus beheersen: stapsgewijze CNC-programmagids
- Fanuc CNC programmeergids: een simpel, functierijk voorbeeld
- Fanuc CNC G81 boorcyclus programma – Stap-voor-stap voorbeeld
- Uitgebreid Fanuc G94 vlakkeercyclus voorbeeld voor CNC-bewerking
- Beginner CNC-nutfrezen programma: Eenvoudig voorbeeld & stap-voor-stap gids
- De G84 Taphulpcyclus beheersen: Praktische CNC-programmeergids
- Fanuc G68 Coördinaten Rotatie G-code Voorbeeld voor CNC Bewerking
- Siemens Sinumerik 4-as freesprogramma: Praktisch CNC-voorbeeld
- Quincunx CNC-plasma snijprogramma voorbeeld: G91 incrementele besturing
- CNC Freesboog Voorbeeld: G2 met I & J Parameters
- Fanuc G68 Coördinaterotatie: Praktisch Subprogramma Voorbeeld